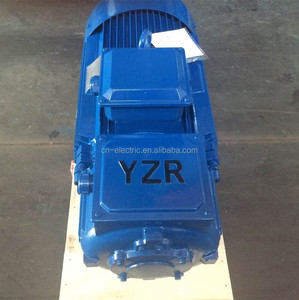
Direct factory-engineered asynchronous motors tested for Australian operating conditions (415V 50Hz, AS/NZS 1359 & MEPS compliance). Request technical datasheets or instant quotes below.
Melbourne remains the manufacturing powerhouse of Australia, spanning heavy industrial corridors from Dandenong South and Campbellfield to the vital logistics hub at the Port of Melbourne and the chemical processing zones in Altona and Geelong. Operating three-phase asynchronous motors within Victoria requires strict alignment with national grid parameters (415V, 50Hz, 3-Phase) and regulatory mandates governed by the Australian Greenhouse and Energy Minimum Standards (GEMS) scheme and AS/NZS 1359 standards.
Industrial buyers across Victoria face unique challenges: high peak energy costs, aggressive decarbonization targets under the Victorian Energy Upgrades (VEU) program, and demanding climatic conditions where ambient summer temperatures in suburban Melbourne frequently top 40°C to 45°C inside industrial plants. Consequently, specifying industrial electric motors demands far more than basic horsepower matching—it requires granular evaluation of thermal endurance, insulation class (Class H/F with Class B temperature rise limits), variable speed drive (VSD) harmonic resilience, and total cost of ownership (TCO).
To provide true information gain for engineering leaders and procurement directors, our senior technical team analyzed suppliers based on five key operational vectors critical to the Melbourne industrial region.
Motors imported into Victoria must comply with AS/NZS 1359.5 for energy efficiency. Suppliers were graded on their active registration in the Australian GEMS database and availability of certified test reports according to IEC 60034-2-1 methods.
Evaluating motor survival under extreme Victorian heatwaves. High marks were awarded for Class H vacuum pressure impregnation (VPI) insulation, tropicproofing treatments, and bearings rated for extended thermal expansion cycles.
Modern Melbourne plants rely heavily on Variable Frequency Drives. We assessed insulated non-drive end (NDE) bearings to prevent fluting, reinforced phase separators, and IC416 forced-cooling options for low-speed continuous torque operations.
Downtime costs in Melbourne bottling lines or cold storage centers can exceed $20,000/hour. Suppliers with ready-to-ship stock in Melbourne metro warehouses (Bayside, Westgate, or Outer East) earned distinct operational points.
Ability to modify shaft dimensions, terminal box positioning, flange configurations (B3, B5, B14), and specialized hazardous area ratings (IECEx Ex d, Ex eb, Ex t) for petrochemical and mining OEM exporters servicing Australasia.
Below is the comprehensive technical benchmark of the leading motor manufacturers, local distributors, and international exporters supplying three-phase induction drives to Victoria.
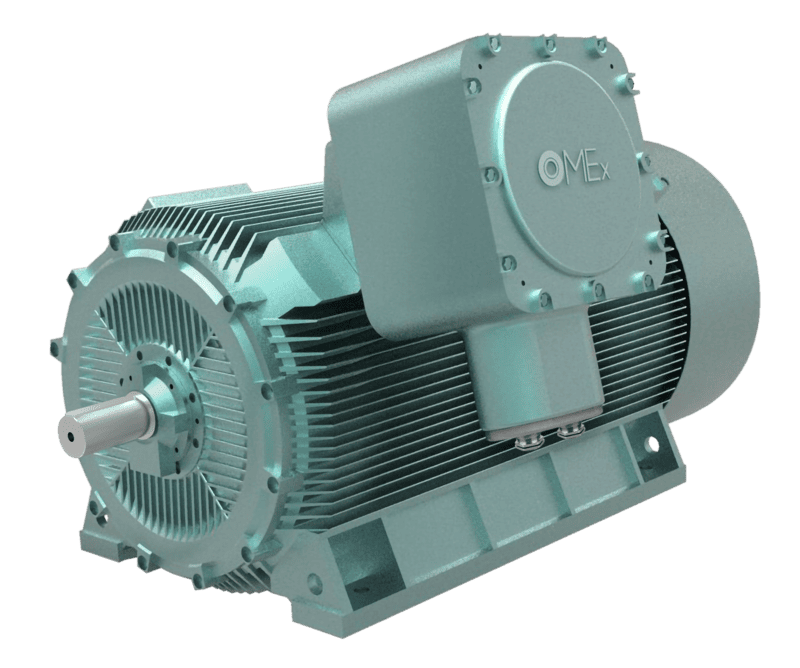
Premier European industrial motor manufacturer specializing in custom heavy-duty, high voltage, and explosion-proof 3-phase asynchronous motors. Engineered with over 50 years of Italian precision, offering direct export supply and customized engineering for complex Victorian municipal and industrial projects.
A dominant player in the Australian industrial automation market, offering standard M3BP and process performance three-phase induction motors with strong local service representation across Victoria.
Known for the SIMOTICS GP and SD series. High reliability for continuous process integration in Melbourne water treatment plants and food production lines requiring precise VFD control.
Extensive local distribution network in Victoria with high availability of W22 cast iron low voltage motors. Popular choice for standard pump and fan industrial retrofits.
Provides a solid range of low-voltage and medium-voltage three-phase asynchronous motors widely utilized in heavy manufacturing and ventilation across Australasia.
Supplies Marathon Electric and heritage GMF motor series to the Australian market. Strong presence in agricultural pumping and standard commercial HVAC fans.
Recognized for rugged motor builds serving heavy industrial infrastructure, power generation, and wastewater management in Victoria.
Headquartered locally in Knoxfield, Melbourne. Specializes in integrated gearmotors, dynamic asynchronous servomotors, and automated drive systems.
A major Asian exporter delivering high-volume YE3/YE4 efficient standard induction motors to Australian original equipment manufacturers (OEMs).
Dynamic manufacturer producing specialized small-to-medium 3-phase asynchronous induction motors optimized for water pump OEMs, compressor skids, and agricultural machinery.
Three-phase asynchronous induction motors form the electromechanical backbone of Melbourne’s core industries. Understanding local application environments is key to correct motor specification.
Utilized across major infrastructure projects managed by Greater Western Water and Yarra Valley Water. Motors drive high-capacity centrifugal pumps, aerators, and sludge mixing impellers. Requires IP66/IP67 epoxy coatings, Class H VPI insulation, and internal anti-condensation heaters to withstand constant humidity and aggressive chemical environments.
In Campbellfield, Dandenong, and Truganina food processing hubs, motors power stainless-steel mixing vessels, industrial refrigeration compressors, and high-speed packaging conveyors. Demand strict compliance with smooth surface designs, washdown protection, and IE4 super-premium efficiency for 24/7 continuous operations.
Container terminals and bulk loading facilities require heavy-duty YZR wound rotor slip ring motors and VFD inverter duty drives. Operating near Port Phillip Bay means motors must feature marine-grade C5-M anti-corrosion paint systems and stainless-steel hardware against aggressive salt spray.
Major infrastructure projects such as the Metro Tunnel and West Gate Tunnel rely on heavy-duty smoke extraction motors. Certified to emergency F300 (300°C for 2 hours) or F400 standards, ensuring non-stop air evacuation during fire hazards alongside standard IE3 air conditioning chiller drives.
Refineries and chemical manufacturing plants operate under hazardous zone classifications (Zone 1 & Zone 2). Motors must be strictly IECEx certified flameproof (Ex d / Ex db) or increased safety (Ex eb) to prevent spark ignition in flammable gas environments.
Across regional Victoria and outer Melbourne quarry sites, high-torque 3-phase motors drive jaw crushers, vibratory screens, and long-distance overland conveyors. Require cast-iron frame construction, reinforced roller bearings, and dust-tight IP65 enclosure sealing.
As Australia advances toward Net-Zero targets, industrial motor selection in Melbourne is undergoing a rapid technological shift driven by three primary economic and regulatory catalysts:
While IE3 is currently the baseline for Australian MEPS compliance, forward-thinking Melbourne manufacturers are increasingly adopting IE4 Super Premium and permanent magnet assisted synchronous reluctance motors. Transitioning a 110kW continuously running pump motor from IE2 to IE4 saves up to 14,000 kWh annually per unit, significantly reducing electricity overheads under Victoria's industrial tariff structures.
The Victorian Government’s VEU scheme provides financial incentives (Victorian Energy Efficiency Certificates - VEECs) when replacing inefficient legacy induction motors with high-efficiency IE3/IE4 motors equipped with VFD controllers. Forward B2B procurement managers leverage these rebates to reduce capital payback periods to under 14 months.
Modern Melbourne plants are mandating smart motor specs. Integrating wireless tri-axial vibration sensors and embedded PT100 resistance temperature detectors (RTDs) directly into the motor windings allows maintenance engineers to catch bearing wear and phase imbalances before sudden catastrophic failure occurs.
Inheriting over 50 years of Italian electromechanical expertise from O.M.E. Motori Elettrici s.r.l. (headquartered in Gussago, Brescia, Italy), OME Motors represents the apex of specialized custom electric motor engineering. While standard off-the-shelf suppliers offer fixed configurations, OME Motors designs tailored solution architectures designed to seamlessly integrate into complex Australian industrial applications.
Our global manufacturing ecosystem adheres strictly to ISO 9001 quality management, ATEX, IECEx, and Australian AS/NZS electrical standards. Whether your plant requires medium-voltage slip ring motors for heavy mill drives, customized dual-speed marine motors, or flameproof explosion-proof motors for oil refineries, OME Motors provides direct engineering support, transparent compliance documentation, and optimized international delivery to Melbourne.
Expert technical answers addressing common installation, standard compliance, and operational queries for engineers operating in Victoria.
The standard nominal low-voltage grid supply in Melbourne and across Australia is 415V at 50Hz (often specified under nominal 400V/415V range). When procuring motors, ensure winding specs match 415V Delta or 690V Star connection options. Standard 380V motors imported from overseas without wide-voltage insulation tolerance (±10%) will run hot and suffer reduced service life on the Australian 415V grid.
Under the Australian Greenhouse and Energy Minimum Standards (GEMS) scheme (AS/NZS 1359.5), all single-speed three-phase cage induction motors rated from 0.73kW up to 185kW sold or installed in Victoria must meet minimum IE3 efficiency levels. Importers and buyers must verify that the motor model is registered in the official GEMS online database prior to installation.
Running a standard 380V rated motor on 415V increases core magnetic flux density by approximately 9.2%. While many quality motors with Class F insulation can tolerate this voltage increase within their ±10% voltage band, it results in higher magnetizing current, elevated operating temperatures, and slightly reduced power factor. It is highly recommended to specify native 415V windings or wide-voltage rated (380-415V) motors for long-term reliability.
Variable Frequency Drives induce common-mode voltages that create high-frequency shaft currents. These currents discharge through the bearings, causing electrical discharge machining (EDM) micro-pitting or "fluting". For motors 55kW and above operating on VSDs in Melbourne facilities, insist on an insulated non-drive end (NDE) bearing or grounding rings to divert damaging shaft currents.
For outdoor installations in coastal Melbourne or damp processing bays (such as Port of Melbourne or Western Treatment Plant), specify a minimum enclosure rating of IP66. This guarantees total protection against dust ingress and high-pressure water jets. Additionally, marine-grade C5-M epoxy paint coatings and 316 stainless-steel hardware are vital to prevent salt spray corrosion.
Industrial plant ambient temperatures during Melbourne summer heatwaves often exceed 40°C. Motors should feature Class H insulation (rated up to 180°C) with design temperature rise limited to Class B (80K). This 45°C thermal reserve margin prevents insulation degradation during prolonged ambient heat events.
For standard 415V supply, dual-voltage motors rated 415V/690V are connected in Delta (Δ) for normal continuous running at 415V. Star (Y) connection is used during reduced-voltage Star-Delta starting to limit high inrush starting current (reducing line voltage surge by a factor of 1/√3). Once up to speed, a timer switch changes the motor to Delta running mode.
Yes. Hazardous areas in chemical, petrochemical (Geelong/Altona), or grain storage handling facilities classified as Zone 1 or Zone 2 under AS/NZS 60079 require certified explosion-proof motors. Australia accepts the IECEx certification scheme. Motors must carry valid IECEx CoC (Certificate of Conformity) documentation stamped directly on the motor nameplate.
IC411 relies on a self-ventilated fan mounted directly on the motor shaft; cooling airflow decreases when the motor is slowed down by a VFD. IC416 utilizes an independent electric cooling fan that maintains maximum airflow regardless of the main motor’s operating speed—essential for constant-torque applications running at low frequencies (e.g., 5-25 Hz).
Standard stock frames can be dispatched from local Victorian warehouses within 24-48 hours. For specialized custom-engineered motors (such as high-voltage OMEX explosion-proof units or slip ring motors), international direct sea freight takes approximately 3 to 5 weeks, while urgent emergency air-freight options can deliver within 7 to 10 working days.
Need assistance sizing a high-efficiency 3-phase asynchronous motor or selecting an IECEx certified drive for your Victorian facility? Speak directly with our senior application engineers.
Get a Quote