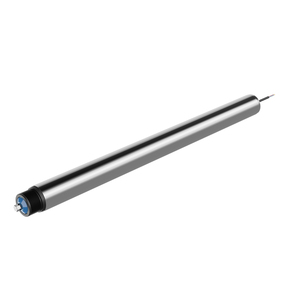
Extremely rugged drum motors designed with arctic-grade synthetic lubricants, Viton double-lip oil seals, and dynamic thermal compensation systems capable of reliable continuous torque at -40°C in underground iron ore operations.
Explosion-proof ATEX Zone 1/21 certified high-voltage and low-voltage heavy conveyor drives with thermal shielding, designed to support Sweden’s pioneering carbon-neutral steel processing and heavy bulk material transfers.
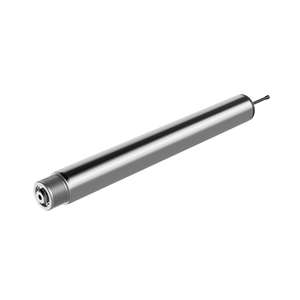
Smart 24V/48V Brushless DC motorized rollers featuring integrated BUS communications (CANopen, EtherCAT) for zero-pressure accumulation (ZPA) sorting in battery assembly facilities and automated distribution hubs.
"In Sweden’s rigorous industrial landscape—spanning subterranean Arctic iron mines in Kiruna to high-speed food packaging lines in Skåne—conveyor belt electric motors must deliver unmatched mechanical resilience, strict eco-design energy compliance (EU 2019/1781), and zero unscheduled downtime."
Selecting the optimal electric drive system for belt conveyors, motorized rollers, and heavy-duty drum pulleys requires a sophisticated understanding of mechanical load profiles, ambient thermal stress, protection ratings (IP65 to IP69K), and localized regulatory frameworks. As a premier custom OEM manufacturer drawing on over 50 years of European electromechanical heritage (aligning with OME Motors’ Italian design precision), we provide Swedish plant engineers and system integrators with purpose-built conveyor motors engineered specifically for the harsh operating environments of Northern Europe.
Sweden presents a distinct matrix of operating challenges that render off-the-shelf conveyor motors inadequate for demanding industrial use-cases. Our OEM engineering team focuses on three core localized requirements:
In northern Sweden (Norrbotten and Västerbotten regions), outdoor ambient temperatures routinely plummet below -30°C, reaching extreme cold spikes of -40°C. Standard motor lubricants coagulate under these conditions, leading to excessive start-up torque spikes, thermal overload trips, and premature gearbox failure. Our OEM conveyor motors for Sweden utilize specialized synthetic polyalphaolefin (PAO) greases, Viton fluoroelastomer seals with low glass transition temperatures, and optional internal anti-condensation heating elements (230V single-phase trickle heaters) to ensure instant, smooth startup under extreme freezing conditions.
Aligned with Sweden’s target of complete carbon neutrality by 2045 and strict adherence to the Swedish Energy Agency (Energimyndigheten) directives under EU Regulation 2019/1781, our electric drum motors and motorized rollers are engineered to IE3 Premium Efficiency, IE4 Super Premium Efficiency, and permanent magnet IE5 Ultra Premium Efficiency classes. By reducing electrical losses in the stator laminations and optimizing copper winding slot fill factors, our drives minimize kilowatt-hour consumption during continuous 24/7 industrial duty (S1 cycle), dramatically lowering life-cycle operating costs under Swedish SE1–SE4 electricity zone dynamics.
Whether exposed to coastal marine humidity, aggressive road salt, acid-generating mineral dust in underground mining, or caustic chemical sanitizers in food processing plants (such as dairy, seafood, and meat processing facilities across southern Sweden), moisture ingress is the primary failure mode of conveyor drives. We offer custom shell treatments including 316L stainless steel enclosures, high-build epoxy coatings certified to ISO 12944 C5-M (Coastal/Industrial Heavy Marine), and dynamic labyrinth seals rated to IP69K (high-pressure, high-temperature washdown resistance).
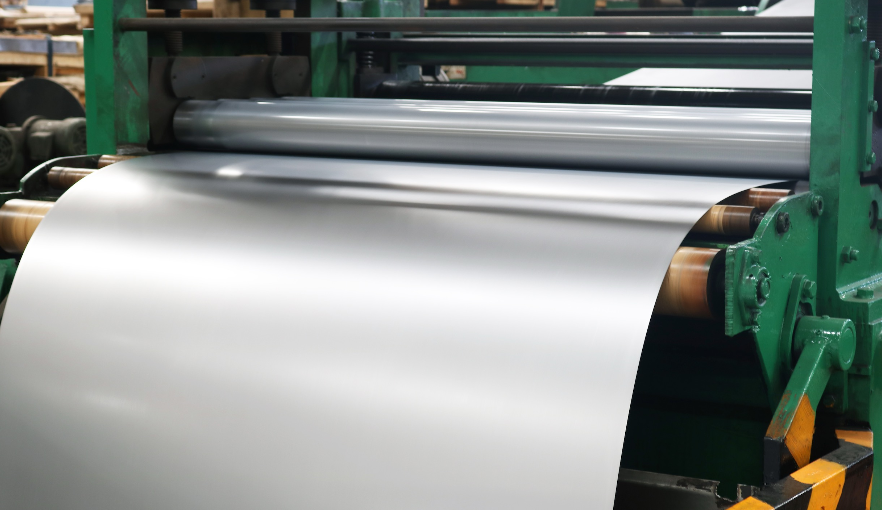 Figure 1: Heavy-duty industrial electric drum motor stator and rotor assembly optimized for high-torque conveyor operations.
Unlike standard modular electric motor suppliers, our OEM manufacturing model provides total dimensional, electrical, and mechanical adaptability. Swedish conveyor OEMs can specify exact motor geometries to drop directly into existing conveying frames (reducing structural retrofit costs).
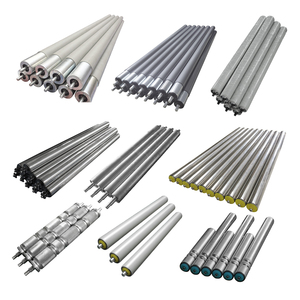
For modern automated logistics hubs, e-commerce distribution centers, and high-tech battery cell manufacturing lines (e.g., Northvolt Gigafactories), traditional 400V tri-phase external geared motors are increasingly replaced by decentralized 24V and 48V DC motorized rollers (MDR). Our ZWG series features high-density brushless DC (BLDC) motors integrated directly inside 50mm, 76mm, and 89mm diameter roller shells. Key technical features include:
For heavy bulk handling—such as crushed stone, gravel, iron ore, bio-fuel pellets, and wood chips—our DL and heavy-duty drum motor series encloses the motor, high-precision planetary gearbox, and bearings completely inside a sealed outer cylindrical pulley shell. Advantages over exposed motor-gearbox-chain arrangements include:
To assist technical procurement teams and plant engineering managers across Sweden in evaluating conveyor drive options, the following comparison matrix details key performance metrics across our three primary OEM drive configurations:
| Specification Parameter | 24V/48V BLDC Motorized Roller | Food-Grade Stainless Drum Motor | Heavy-Duty Mining/ATEX Drum Motor |
|---|---|---|---|
| Target Application | Logistics, Parcel Sorting, Battery Lines | Food, Dairy, Meat & Pharma Packing | Mining, Steel Mills, Bulk Aggregates |
| Voltage Options | 24V DC / 48V DC Safe Extra-Low Voltage | 1x230V, 3x400V / 460V 50/60Hz | 3x400V, 3x690V 50Hz (Inverter Duty) |
| Power Range | 30W to 150W Per Roller | 0.18 kW to 7.5 kW | 5.5 kW to 132 kW Heavy Duty |
| Ingress Protection | IP65 / IP66 Standard | IP67 / IP69K High-Pressure Washdown | IP66 / IP67 Hermetic Cast Iron |
| Shell Material & Finish | Zinc-Plated Steel / Aluminum / Rubber | 316L Polished Stainless Steel (Ra < 0.5 µm) | Heavy Cast Iron / Rubber Lagging (V-Groove) |
| Explosion Proof Rating | Non-Ex (Standard Clean Room) | Optional ATEX Dust Zone 22 | ATEX Ex d IIB T4 / IECEx Zone 1, 21, 2, 22 |
| Operating Temperature | -10°C to +40°C | -25°C to +50°C (FDA Synthetic Oil) | -40°C to +60°C (Arctic Grease & Heaters) |
 Figure 2: Precision-balanced high-torque conveyor motor rotors undergoing rigorous quality control testing for heavy continuous industrial operation.
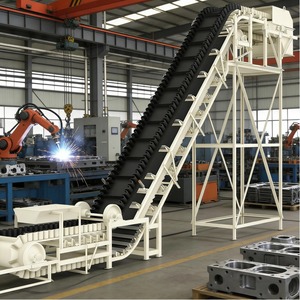
Underground mining operations require conveyor motors capable of handling brutal shock loads when heavy iron ore or copper aggregates crash onto high-angle incline belts. Our heavy-duty drum motors feature case-hardened alloy steel planetary gear trains (exceeding AGMA 12 rating), heavy-wall steel drums with hot-vulcanized diamond-pattern rubber lagging, and dual thermal protection (PT100 resistance temperature detectors and PTC thermistors integrated directly in the stator windings). Furthermore, ATEX Ex d certification ensures safe operation in coal/dust laden shaft pockets where explosive dust atmospheres may accumulate.
Sweden’s transition to fossil-free steel production requires conveyor systems operating in proximity to high-temperature reduction furnaces, pelletizing plants, and sinter lines. Our high-voltage and low-voltage heavy-duty drum drives are engineered with Class H insulation systems (capable of withstanding internal hot-spot temperatures up to 180°C) and water-cooled outer jacket option (IC81W/IC611 cooling configurations) to isolate the electrical stator from intense radiant ambient heat.
In Swedish food production (such as meat packing plants in Malmö or fish processing in Gothenburg), high-pressure chemical washdowns with chlorine or caustic soda are performed daily. Standard external geared motors rust quickly, and open belt pulleys trap food particles, inviting bacterial contamination (such as Listeria). Our food-grade PU and modular belt drum motors feature smooth, cylindrical 316L stainless steel shells without cooling fins, external bolts, or keyways where debris can lodge. Sealed with food-grade NSF H1 registered synthetic lubricants, they fully comply with EHEDG and FDA regulations.
Forward-thinking Swedish procurement managers are prioritizing three structural technological trends when specifying next-generation electric conveyor drives:
Rather than relying on reactive repairs or fixed time-based maintenance schedules, modern Swedish smart factories demand real-time telemetry. Our custom OEM drum motors can be equipped with embedded IO-Link vibration sensors, 3-axis accelerometer chips, and digital moisture detection probes inside the oil chamber. If bearing wear or seal degradation occurs, the drive sends an alert over PROFINET directly to the plant's SCADA or maintenance dashboard before catastrophic failure happens.
Fixed-speed conveyor operations are rapidly declining in Sweden as plants optimize material throughput dynamically. Our conveyor motors feature inverter-duty magnet wire with spike-resistant corona-proof insulation (capable of handling high dV/dt voltage transients from modern PWM variable frequency drives). Combined with insulated non-drive end bearings (or ceramic hybrid bearings), shaft current erosion and electrical discharge machining (EDM) pitting are totally eliminated.
Drawing on over 50 years of electromechanical innovation (inheriting the design tradition of O.M.E. Motori Elettrici s.r.l.), our manufacturing facilities combine rigorous European quality assurance with modern automated production. Every conveyor motor bound for Sweden undergoes 100% routine testing including high-voltage insulation tests, dynamic rotor balancing, oil-seal pressure leak tests, and no-load performance verification.
Whether you require a single high-torque replacement drum motor for an iron ore conveyor in Kiruna or 5,000 low-voltage motorized rollers for an automated parcel sorting hub in Stockholm, our engineering desk works side-by-side with your technical team to optimize performance, energy efficiency, and overall operational reliability.
Speak directly with our senior electromechanical engineering team today. Get technical datasheets, CAD 3D models, energy efficiency calculations, and customized OEM pricing within 24 hours.