Explore our top-tier CE-certified three-phase asynchronous motors designed for continuous S1 duty cycle, featuring 100% electrolytic copper windings, cast iron frames, and IP55/IP66 enclosure protection.
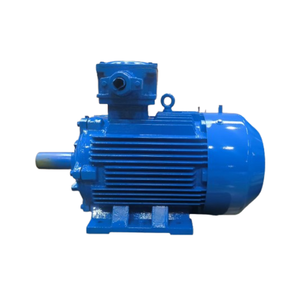
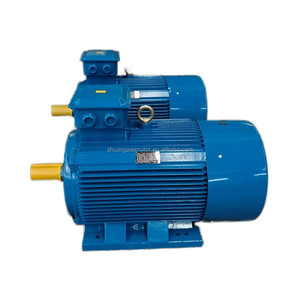
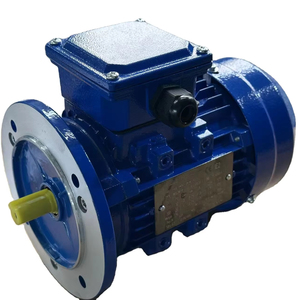
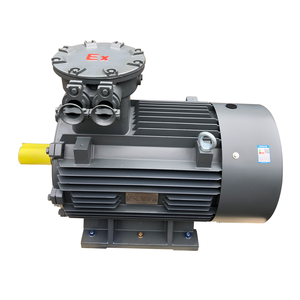
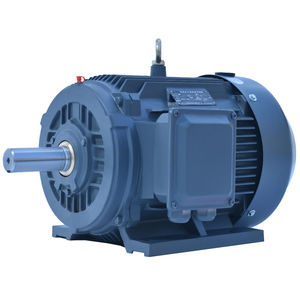
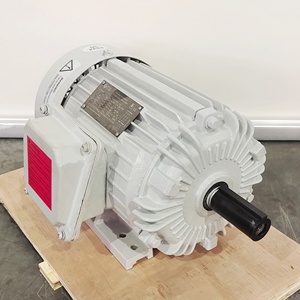
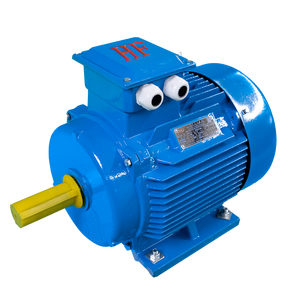
As an authoritative global manufacturer of CE Certified Squirrel Cage Induction Motors, our factory engineers every three-phase asynchronous motor with meticulous attention to electromagnetic design, thermal endurance, and mechanical structural integrity. In Australian industrial operations, electric motors consume over 60% of total electrical power in sectors such as mineral beneficiation, water pumping, bulk material conveyance, and heavy HVAC installation.
A squirrel cage induction motor derives its name from its rugged, short-circuited rotor structure resembling a squirrel cage wheel. The rotor consists of longitudinal copper or aluminum conductive bars embedded into laminated steel slots and permanently short-circuited at both ends by heavy-duty conductive end rings. When connected to a standard Australian 415V 50Hz three-phase supply, the stator windings generate a rotating magnetic field ($N_s = 120f/P$). This magnetic flux cuts across the shorted rotor bars, inducing heavy electromotive force (EMF) and rotor currents that produce high starting and breakdown torque without requiring brushes, slip rings, or internal electronic commutators.
| Technical Parameter | Standard Global Baseline | Our Australian Specification Standard | Operational Advantage in Australia |
|---|---|---|---|
| Rated Voltage & Frequency | 380V / 50Hz or 460V / 60Hz | 415V / 50Hz (Tolerance ±10%) | Eliminates thermal overload and saturation risks under Australian grid voltage fluctuations. |
| Insulation & Thermal Class | Class F Insulation (105°K rise) | Class H VPI Resin Insulation (80°K rise) | Extends motor lifespan by 2.5× under continuous 50°C ambient temperatures. |
| Ingress Protection (IP) | IP54 / IP55 Standard | IP55 Standard, IP65 / IP66 Optional | Prevents micro-fine iron ore dust, red mud, and high-pressure water washdowns from penetrating frame. |
| Efficiency Benchmark | IE2 Standard Efficiency | IE3 Premium & IE4 / IE5 Super Premium | Full compliance with Australian MEPS (AS/NZS 1359.5), slashing operating energy expenses. |
| Conductor & Winding | Standard Copper / CCA Options | 100% Oxygen-Free Electrolytic Copper | Minimizes $I^2R$ copper losses, maximizing motor shaft power conversion efficiency. |
To eliminate cogging, reduce magnetic noise, and smooth out harmonic torque pulsations during starting, our engineering team utilizes computer-optimized rotor slot skewing. By positioning the rotor slots at a calculated angle relative to the shaft axis, harmonic voltages induced by stator slot teeth are neutralized. This structural refining leads to an ultra-quiet acoustic profile (below 72 dB(A) at 1 meter), reduced bearing vibration amplitudes compliant with ISO 10816-1 Grade A, and superior low-speed torque stability under Variable Frequency Drive (VFD) operation.
Insulation failure is the leading root cause of industrial motor burnouts in remote Australian sites where humidity, salt fog, and chemical fumes degrade dielectric strength. Our factory deploys a state-of-the-art Vacuum Pressure Impregnation (VPI) process utilizing solventless Class H epoxy resin. The assembled stator core undergoes deep vacuum evacuation to pull out all air pockets trapped within the winding slots, followed by high-pressure resin injection and thermal baking curing.
From remote Western Australian mines to high-capacity agricultural irrigation in the Murray-Darling Basin, our squirrel cage induction motors are customized to overcome extreme environmental stresses.
Pilbara iron ore mines, gold processing plants, and coal washeries represent some of the world's harshest industrial environments. Our heavy-duty cast iron YE3 and IE4 motors feature IP66 dust-tight sealing, regreasable SKF/NSK bearings, and reinforced bearing end-shields to drive jaw crushers, vibrating screens, slurry pumps, and heavy overland belt conveyors without thermal or mechanical failure.
Agricultural pump stations along the Murray-Darling basin and rural regional water authorities require continuous 24/7 S1 operating capability. Our 100% copper wound 4-pole and 6-pole squirrel cage motors are equipped with rain covers (canopies), anti-condensation heaters, and high thrust bearings specifically configured for deep-well turbine pumps, centrifugal irrigation pumps, and wastewater aeration impellers.
Operating in maritime environment ports such as Newcastle, Port Hedland, and Gladstone exposes equipment to extreme C4/C5-M atmospheric corrosivity. We supply custom marine-duty squirrel cage motors painted with multi-layer epoxy resin systems (coating thickness >240μm), 316 stainless steel fasteners, external brass earth studs, and IP66 double-lip viton oil seals to guarantee long-term integrity.
For Australian chemical processing plants, underground coal mines, oil refineries, and grain handling facilities where explosive gases (Zone 1/2) or combustible dusts (Zone 21/22) are present, our IECEx and ATEX certified flameproof Ex d IIB T4 / Ex tD induction motors offer certified containment against internal explosion propagation.
Building services engineers across Sydney, Melbourne, and Brisbane require compliant dual-duty ventilation motors. Our high-temperature smoke spill extraction motors operate continuously as standard HVAC fan drives at normal temperatures, while certified to run at 300°C or 400°C for up to 2 hours (F300/F400 emergency rating) during building fire events.
In steel mills, foundry casting plants, and cement works, induction motors face continuous thermal shock and extreme mechanical radial loads. Our IE4 Permanent Magnet and heavy cast-iron squirrel cage motors deliver massive breakdown torque ratios ($T_k/T_n \ge 3.0$), protecting machinery from stalling under sudden overload spikes.
Australian industrial procurement managers and original equipment manufacturers (OEMs) operate under stringent energy performance mandates. The Greenhouse and Energy Minimum Standards (GEMS) Act enforces Minimum Energy Performance Standards (MEPS) specified in AS/NZS 1359.5 for three-phase electric motors rated from 0.73kW to 185kW.
With industrial electricity tariffs in Australia rising rapidly, electricity cost over a motor's 15-year operational lifecycle represents up to 95% of its Total Cost of Ownership (TCO). Upgrading an older IE1 or IE2 motor fleet to our IE4 Super Premium Induction Motors or IE5 Permanent Magnet Motors cuts energy consumption by 4% to 12%, achieving complete capital expenditure ROI within 8 to 14 months of continuous operation.
Modern Australian processing facilities extensively utilize Variable Frequency Drives (VFDs) for process speed automation. To prevent bearing fluting and premature lubricant breakdown caused by shaft voltage discharge, our motors offer optional insulated non-drive end (NDE) bearings, shaft grounding rings (SGR), and inverter-grade magnetic wire with spike-resistant varnish compliant with IEC 60034-25.
Below is a comparative data model demonstrating the direct financial savings of deploying a 75kW 4-Pole IE4 Super Premium Squirrel Cage Induction Motor versus a standard IE2 motor in an Australian mining application operating 8,000 hours per year at an average energy rate of AUD $0.22 / kWh:
| Evaluation Parameter | Standard IE2 Induction Motor | Our IE4 Super Premium Motor | Annual Financial Difference (AUD) |
|---|---|---|---|
| Nominal Motor Efficiency | 94.0% Efficiency | 96.2% Super Premium Efficiency | +2.2% Absolute Efficiency Gain |
| Input Electrical Power Required | 79.79 kW | 77.96 kW | 1.83 kW Power Demand Reduction |
| Annual Energy Consumption (8000 hrs) | 638,320 kWh | 623,680 kWh | 14,640 kWh Saved / Year |
| Annual Energy Expenditure (@ $0.22/kWh) | AUD $140,430 | AUD $137,210 | AUD $3,220 Net Savings / Year |
| 10-Year Cumulative Carbon / Cost Benefit | AUD $1,404,300 | AUD $1,372,100 | AUD $32,200 Savings + 120t $CO_2$ Avoided |
Combining over 50 years of European electromechanical engineering lineage with a state-of-the-art high-capacity manufacturing base, we supply reliable squirrel cage induction motors with direct factory support.
Every motor dispatched to Australia carries valid CE marks, IECEx compliance certificates, and full routine test reports. ISO 9001 and ISO 14001 certified quality control ensures complete batch traceability.
We supply non-standard shaft extensions (tapered, double-ended, keyless), custom mounting flange dimensions (B3, B5, B14, B35, V1), specialized terminal box positionings (Top, Right, Left), and built-in PT100 temperature sensors.
We never compromise on rotor or stator conductors. Our coils use Grade H 200°C rated enamel-insulated pure copper wire, ensuring maximum overload capacity and superior heat dissipation.
With massive raw material inventories and streamlined automated CNC rotor-stator punching lines, we guarantee fast manufacturing turnarounds and direct sea/air freight logistics to Sydney, Melbourne, Brisbane, Fremantle, and Adelaide ports.
Clear, technical answers to common queries regarding grid compatibility, MEPS regulations, enclosure standards, and custom factory modifications.
Get direct-from-factory pricing, full engineering datasheets, dimensional 2D/3D CAD models, and customized electromechanical solutions tailored for Australian industrial projects.