Explore our top-tier asynchronous, permanent magnet, and explosion-proof high voltage motor systems engineered for hazardous industrial environments.
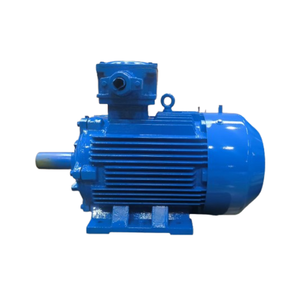
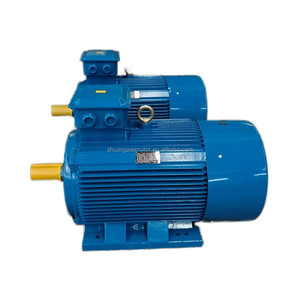
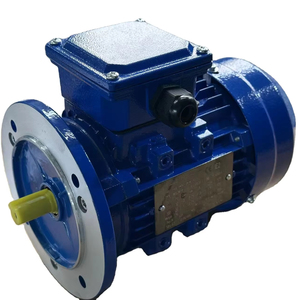
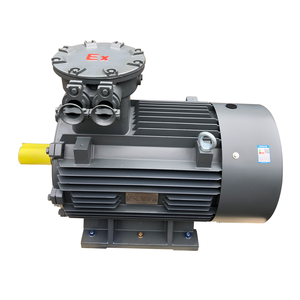
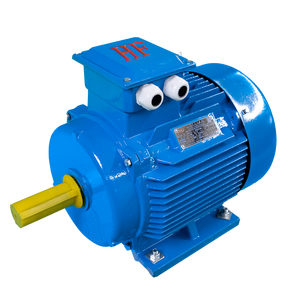
Flameproof High Voltage Motors represent the pinnacle of severe-duty electrical engineering. Designed to operate safely in volatile atmospheres containing explosive gases, vapors, or combustible dusts (Zone 1, Zone 2, Class I Division 1/2 environments), these machines are critical power drives across global oil refineries, offshore platforms, underground mines, chemical processing units, and power plants.
Unlike standard industrial motors, a flameproof (Ex d or Ex db certified under IEC/EN 60079-1 standards) motor is constructed to contain an internal explosion without transmitting the resulting flame, hot gases, or sparks to the surrounding flammable atmosphere. When selecting a trusted flameproof high voltage motor manufacturer, EPC project managers and procurement directors must evaluate complex thermodynamic, electrical, and mechanical insulation integrity specs.
Key Design Integrity Rule: The flameproof enclosure does not prevent explosive gas from entering the internal motor chassis. Instead, it relies on precisely calculated flamepaths (flange, spigot, or threaded joints) that cool hot escaping combustion gases below the auto-ignition threshold of the surrounding ambient gas group (such as IIA, IIB, or IIC / Hydrogen).
A primary benchmark of high-voltage flameproof motor manufacturing is structural tensile strength. The cast iron or fabricated heavy-plate steel enclosure must withstand internal hydrostatic explosion pressures exceeding 1.5 times the maximum theoretical reference pressure (typically tested up to 15 to 20 bar). Flamepaths are engineered with microscopic tolerances (gaps under 0.15 mm to 0.20 mm depending on gas group) and extended joint lengths, ensuring thermal energy dissipation as gases vent outwards.
Operating at medium and high voltage ratings (3.3kV, 6.6kV, 10kV, up to 13.8kV), electrical stress inside the stator windings can trigger partial discharge (PD) or electrical treeing if micro-voids exist. Premier manufacturers utilize Vacuum Pressure Impregnation (VPI) with solventless epoxy resin, integrated with Class H/F mica tape insulation. This process guarantees void-free thermal dissipation, mechanical resistance against electromagnetic surges, and protection against moisture and corrosive chemical ingress.
Our engineering framework integrates advanced thermal management, certified enclosure integrity, and ultra-high efficiency rotor design.
Independently certified by notified bodies (TÜV, CESI, Eurofins) for Ex db / Ex eb protection modes. Engineered for global deployment across European, Middle Eastern, Asian, and American industrial installations.
Available in multiple cooling configurations: Totally Enclosed Fan Cooled (IC411), Air-to-Air Heat Exchanger (IC611), or Air-to-Water Heat Exchanger (IC81W) to optimize thermal profiles under continuous heavy loads.
Strengthened phase insulation and insulated bearings (or shaft grounding rings) eliminate destructive bearing currents (EDM) and withstand steep voltage rise rates (dV/dt) caused by modern PWM Variable Frequency Drives.
Below is a detailed engineering matrix detailing standard technical parameters provided by leading flameproof high voltage motor factories:
| Technical Parameter | Low Voltage Ex d Series | Medium Voltage Ex d (IC411) | High Voltage Ex d (IC611 / IC81W) |
|---|---|---|---|
| Power Output Range | 0.75 kW – 375 kW | 160 kW – 2,000 kW | 1,000 kW – 15,000 kW+ |
| Rated Supply Voltage | 380V / 400V / 690V / 1000V | 3.3 kV / 6.6 kV | 6.6 kV / 10 kV / 11 kV / 13.8 kV |
| Explosion Protection Class | Ex db IIB / IIC T4 Gb | Ex db IIB / IIC T4 Gb | Ex db IIB / IIC T4 Gb or Ex eb / Ex pxb |
| Efficiency Standard | IE3 / IE4 / IE5 Permanent Magnet | IE3 / IE4 High Efficiency | Custom High Efficiency Optimization |
| Protection & Insulation | IP55 / IP56 / IP66; Class F/H | IP55 / IP65; Class H (VPI) | IP55 / IP56; Class H (VPI with Mica) |
| Ambient Temperature Range | -20°C to +40°C (Ext: -50°C to +60°C) | -40°C to +55°C | -50°C to +60°C Extreme Duty |
| Primary Applications | Chemical Pumps, Blowers, Mixers | Refinery Compressors, Large Fans | Pipeline Pumping, Mine Hoists, Power Plants |
The industrial electric motor market is experiencing a profound transition driven by global decarbonization mandates, stricter environmental safety directives, and digital transformation. B2B procurement managers and plant engineering leaders must navigate several evolving procurement trends when selecting flameproof high voltage motor partners:
Electricity accounts for over 90% of an industrial motor's Total Cost of Ownership (TCO) over a 20-year operational lifecycle. Facilities are replacing legacy IE2/IE3 asynchronous units with Permanent Magnet Synchronous Motors (PMSM) capable of achieving IE4 and IE5 energy ratings even in hazardous Ex environments, resulting in millions of kilowatt-hours saved annually.
Modern flameproof motors now feature non-intrusive, ATEX-certified vibration sensors, bearing temperature detectors (PT100), and partial discharge monitoring nodes. Real-time telemetry allows predictive maintenance algorithms to flag bearing fatigue or insulation breakdown long before catastrophic downtime occurs.
Global energy projects are expanding into severe climatic zones—from arctic LNG terminals experiencing -50°C freeze cycles to Middle Eastern desert refineries with ambient temperatures exceeding +55°C. Top manufacturers provide specialized steel alloys, anti-corrosive marine C5-M painting systems, and internal space heaters.
Industrial buyers prioritize OEM manufacturers capable of modular manufacturing. Standardized terminal box positions, interchangeable mounting dimensions (B3, B5, V1), and global spare parts warehouses ensure rapid lead-time delivery and reduced emergency maintenance inventory overhead.
Drawing upon more than 50 years of Italian electromechanical expertise, OME Motors (O.M.E. Motori Elettrici s.r.l.) stands as a premier worldwide manufacturer of custom industrial electric motors. Combining heritage precision from our manufacturing roots in Gussago and Nuvolera, Italy, with global distribution capabilities, our facilities supply heavy-duty motors trusted by fortune-500 energy and infrastructure leaders.
Our flameproof high voltage motor manufacturing operations adhere strictly to rigorous international quality control frameworks. Every single unit undergoes rigorous Factory Acceptance Testing (FAT) prior to shipment, ensuring complete operational readiness under severe environmental stresses.
Full-load testing, hydrostatic pressure tests up to 20 bar, partial discharge verification, dynamic rotor balancing (Grade G1.0/G2.5), and noise/vibration spectrum analysis.
Tailored shaft extensions, special flange dimensions, custom terminal box configurations, dual-shaft extensions, and retrofitting existing obsolete motor dimensions.
Comprehensive technical assistance, commissioning support, emergency spare parts supply, and localized service center coverage across Europe, America, Middle East, and Asia.
Answers to essential technical and procurement questions concerning high voltage flameproof motor selection and compliance.
An Ex d (Flameproof) motor is built with an explosion-proof enclosure designed to withstand internal gas ignition and cool escaping gases via calibrated flamepaths so they cannot ignite external flammable atmospheres. An Ex e (Increased Safety) motor does not contain an internal explosion; instead, it utilizes elevated safety factors (stricter clearance distances, lower temperature limits, enhanced insulation) to prevent any arcs, sparks, or excessive temperatures from occurring during normal operation.
Yes, but they must be specifically certified for VFD operation under combined motor-drive testing or thermal protection parameters (using embedded PTC or PT100 sensors). VFDs introduce high voltage peaks (dV/dt) and harmonic distortion. To protect the motor, manufacturers apply reinforced VPI insulation, insulated non-drive end bearings to stop bearing currents, and external forced cooling fans (IC416) if operating at low speeds under constant torque.
Standard industrial motors are typically rated for -20°C to +40°C. However, severe-duty flameproof high voltage motors manufactured for extreme environments can be engineered for temperatures as low as -50°C (utilizing special ductile iron or forged steel frames that avoid brittle fracture) and up to +60°C (utilizing de-rated thermal designs and Class H insulation systems).
IC611 uses an air-to-air heat exchanger mounted on top of the motor; internal warm air circulates through tubes while an external fan blows ambient air over the tubes to dissipate heat. IC81W uses an air-to-water heat exchanger where cooling water is piped through the heat exchanger. IC81W provides significantly higher cooling density, resulting in a more compact motor footprint for high megawatt ratings, ideal where clean industrial cooling water is available.
Standard delivery packages include ATEX / IECEx Certificates of Conformity, EU Declaration of Conformity, Factory Acceptance Test (FAT) reports, VPI insulation withstand certificates, dimensional footprint drawings, 3D CAD files, operation and maintenance manuals, and certified noise/vibration test records.
Connect directly with our senior application engineers to review your electrical motor specifications, environmental requirements, and custom frame designs.
Send an Inquiry