Precision-engineered electric motors configured for extreme industrial environments, petrochemical processing, oil pipelines, and heavy-duty machinery.
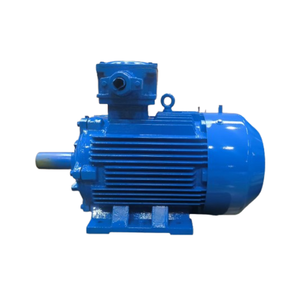
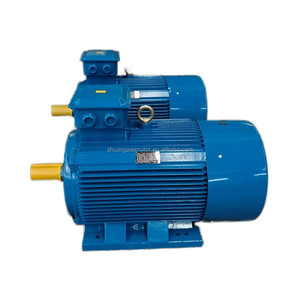
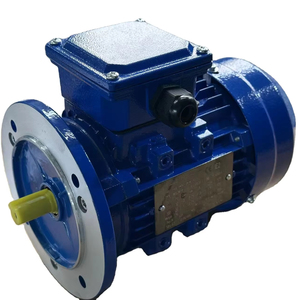
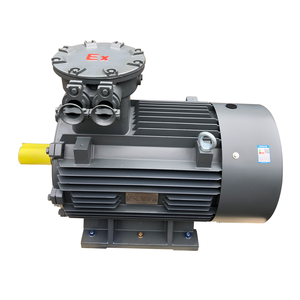
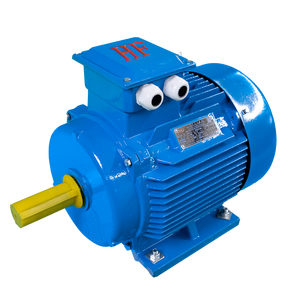
In modern heavy chemical processing, oil refineries, offshore drilling platforms, underground mining operations, and grain storage handling facilities, the presence of flammable gases, vapors, mists, and combustible dusts creates volatile operating environments. Selecting the appropriate CE Certified ATEX Explosion Proof Motor is not merely a regulatory prerequisite under EU Directive 2014/34/EU—it is a critical life-safety parameter and an operational reliability imperative.
Rooted in over 50 years of Italian electromechanical manufacturing excellence, our enterprise integrates deep metallurgical expertise, precision flamepath machineries, advanced electromagnetic design, and stringent quality control protocols. Every explosion-proof motor produced within our specialized manufacturing hubs in Gussago and Nuvolera (Brescia, Italy) undergoes rigorous destructive and non-destructive hydrostatic flameproof testing to guarantee total explosion containment.
| Protection Type | IEC/ATEX Code | Operating Principle | Typical Industrial Hazardous Zone |
|---|---|---|---|
| Flameproof Enclosure | Ex d / Ex db | Contain internal explosion; cool exiting flame through calibrated joint clearances. | Zone 1, Zone 2 (Gas Groups IIA, IIB, IIC) |
| Increased Safety | Ex e / Ex eb | Prevent internal sparks, arcs, or excessive thermal hot-spots during normal and fault operation. | Zone 2 (Gas Groups IIA, IIB, IIC) |
| Non-Sparking | Ex nA / Ex ec | Eliminate risk of sparking contacts or high surface temperatures during normal operation. | Zone 2 (Gases & Vapors) |
| Dust Ignition Protection | Ex tb / Ex tc | Hermetically sealed IP65/IP66 enclosure preventing ingress of combustible dust particles. | Zone 21, Zone 22 (Dust Groups IIIA, IIIB, IIIC) |
Leveraging five decades of electromechanical innovation from our Italian manufacturing facilities, we maintain a complete end-to-end industrial ecosystem ranging from raw material metallurgy selection to final load-testing under simulated field conditions.
Utilizing high-grade electrolytic copper wire coated with Class H double-layered enamel insulation to withstand thermal spikes up to 180°C and prolong motor operational lifespan.
Heavy-duty ribbed GG25/GGG40 grey and ductile iron castings engineered for maximum mechanical strength, high thermal dissipation, and structural integrity under internal overpressure.
Fully certified under ATEX Directive 2014/34/EU, IECEx international scheme, CE conformity, ISO 9001:2015 quality management, and UL/CSA/GOST standard availability.
Equipped with reinforced phase insulation, insulated bearings, and PTC thermistors to eliminate high dv/dt voltage spike damage caused by fast-switching Variable Frequency Drives.
Multilayer polyurethane surface coating systems tested for 1,440 hours of salt spray exposure, protecting motors operating on offshore oil rigs and coastal refineries.
Tailor-made shaft dimensions, special flange mountings (B3, B5, B14, B35), dual-terminal box configurations, space heaters, and specialized encoder retrofits.
The global industrial electric motor landscape is experiencing a paradigm shift driven by stringent decarbonization mandates, rising energy costs, and digital transformation. B2B procurement managers and plant engineers evaluating ATEX explosion-proof motors must align their procurement strategies with several major ongoing technological vectors:
Under regulations such as EU EcoDesign Directive (EU) 2019/1781, energy efficiency mandates are expanding to explosion-proof motors. Industrial buyers are transitioning from traditional IE2/IE3 motors to IE4 Permanent Magnet Synchronous Motors (PMSM) to reduce Total Cost of Ownership (TCO), as electricity accounts for over 90% of a motor's lifecycle cost.
Modern explosion-proof motors are increasingly equipped with intrinsic safety (Ex i) wireless sensors for real-time vibration analysis, bearing thermal tracking, and magnetic flux monitoring. Predictive maintenance algorithms detect bearing wear or winding degradation weeks before catastrophic failure occurs, preventing unplanned refinery shutdowns.
Procurement teams are moving away from evaluating initial CAPEX alone. A high-efficiency Ex d motor operating continuously for 8,000 hours per year will consume its purchase price in electricity within 6 to 12 months. Implementing IE4/IE5 flameproof motors delivers substantial payback over a 15-year operational lifecycle.
Engineering explosion-proof motors requires balancing electromechanical output with strict thermodynamic and explosion-containment boundaries. Recent advancements in material science and computer-aided thermal simulation have unlocked significant performance improvements:
Comprehensive guidance for procurement specialists, electrical engineers, and maintenance managers.
Consult with our senior electromechanical engineering team to select, configure, and specify the exact CE & ATEX certified explosion-proof motor solution for your industrial application.